Aluminum Prototype Machining: A Guide for Pallet and Material Handling Equipment
Aluminum prototype machining is the controlled process of producing functional pallet and material handling components from aluminum stock using CNC milling, turning, drilling, and related finishing operations. I recommend it when an engineering team needs to validate fit, movement, load interfaces, or assembly details before committing to production tooling. For most pallet equipment projects, the best result comes from matching the aluminum grade, machining process, tolerance scheme, surface finish, and inspection method to the actual operating conditions rather than selecting a material by price alone.
Please visit our website for more information on this topic.
At Cornerstone, we approach an aluminum prototype as a manufacturing test article, not simply as a quickly cut sample. We review the part geometry, handling loads, mating surfaces, fastening method, corrosion exposure, and expected quantity before proposing a machining route. This guide explains how buyers can make those decisions and prepare a clearer inquiry for a custom aluminum machining supplier.
Who This Guide Is For
This guide is intended for designers, purchasing teams, equipment manufacturers, and automation integrators developing pallets, conveyor fixtures, transfer plates, guide components, positioning brackets, or other material handling equipment. It is especially relevant when a part must be checked in a real assembly before production quantities are confirmed. It can also help buyers compare prototype machining with fabricated, cast, or standard off-the-shelf alternatives.
I focus on practical decisions that affect function and sourcing: material selection, machining access, tolerances, surface protection, inspection, quantity, and communication with the supplier. These considerations apply whether the prototype is a single design-verification part or a small pilot batch for line testing. The final specification should always be confirmed against the equipment’s actual loads, environment, and safety requirements.
What Aluminum Prototype Machining Involves
Basic Concept and Common Processes
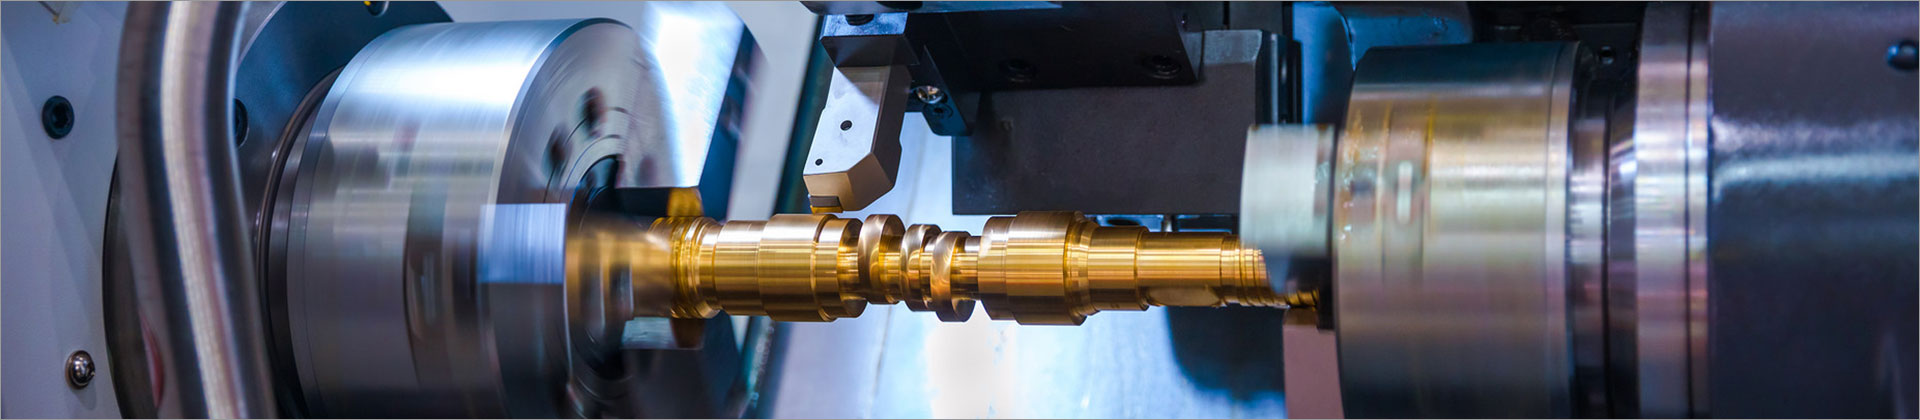
CNC machining removes material from an aluminum billet, plate, bar, or extrusion to create the required geometry. CNC milling is commonly used for pallet plates, brackets, fixture bodies, locator blocks, and mounting structures, while turning is suitable for pins, bushes, spacers, and cylindrical interfaces. Drilling, tapping, reaming, countersinking, deburring, and surface finishing may be combined in the same project.
Aluminum is attractive for prototypes because its density is approximately 2.7 g/cm3, which is substantially lower than many steels. Lower mass can make a manually handled fixture easier to move, but weight reduction does not automatically mean adequate stiffness or load capacity. I therefore treat wall thickness, rib design, unsupported span, fastener location, and contact area as engineering decisions rather than relying on material selection alone.
Material and Specification Overview
6061-T6 is a common starting point for general-purpose machined components because it offers a practical balance of machinability, strength, and availability. 7075 aluminum may be considered when higher strength-to-weight performance is needed, although its cost, corrosion considerations, and suitability for welding or finishing should be reviewed. 5052 or other sheet-oriented alloys can be relevant when the design is based on formed sheet rather than a fully machined billet.
The correct choice depends on the application and not only on the alloy name. A pallet component exposed to moisture, cleaning chemicals, impact, or repeated clamping may require a different evaluation from an indoor positioning bracket. I ask buyers to identify the required alloy temper, any restricted substances or process requirements, and whether welding, anodizing, painting, or other secondary operations will be used.
Key Specifications to Define
A complete drawing should identify critical dimensions, datums, hole sizes, threads, edge conditions, surface finish, material, heat treatment, and inspection requirements. It should also distinguish functional tolerances from non-critical dimensions so that the supplier can control cost without weakening the design intent. As a reference point, a general machined tolerance such as ±0.10 mm may be achievable for many features, but the applicable value must be confirmed for the geometry, size, machine capability, and inspection plan.
Surface finish should be specified by function. A sliding or locating surface may need a smoother finish than a concealed structural face, while an anodized surface can change dimensions and affect the fit of holes or mating parts. If a coating is required, I recommend identifying whether the dimensions apply before or after finishing and whether masking areas must be controlled.
| Decision Area |
Questions to Confirm |
Why It Matters |
| Material |
Which alloy, temper, and stock form are required? |
Strength, machinability, corrosion behavior, and cost can vary. |
| Geometry |
Are there deep pockets, thin walls, or difficult internal corners? |
These features influence tooling, rigidity, cycle time, and risk. |
| Interfaces |
Which holes, datums, and faces control assembly? |
Critical features need clearer tolerances and inspection priority. |
| Finish |
Is anodizing, deburring, brushing, or another finish required? |
Finish affects appearance, corrosion resistance, and dimensional fit. |
Matching the Process to Pallet and Handling Applications
Fixtures, Locators, and Guide Components
Machined aluminum is well suited to prototype fixtures that require accurate hole patterns, repeatable locating surfaces, and quick design changes. For a locator block or guide component, I would prioritize datum control, perpendicularity, edge radii, and the relationship between holes and contact faces. A visually accurate prototype can still fail in service if its locating features do not reference the same datums as the production assembly.
For pallet plates and transfer fixtures, the design review should include load direction, unsupported span, fastener pull-out, impact points, and contact with conveyors or workholding devices. Aluminum can reduce handling mass, but a thin plate may deflect under a concentrated load even when its static strength appears acceptable. Where loads are uncertain, the prototype should be tested under defined conditions by the equipment owner rather than described as universally load-rated.
Small Batches and Design Validation
Prototype machining is valuable when the geometry is still changing or when only a limited number of parts is required for fit and function testing. It avoids the upfront commitment associated with dedicated dies, molds, or other production tooling. However, the machining strategy used for a prototype may not be the lowest-cost strategy for a high-volume production part, so I recommend treating the prototype as a source of manufacturing information for the next stage.
If you are looking for more details, kindly visit cornerstone.
When a design is likely to move into production, I ask the buyer to identify which features are expected to remain stable. This allows us to consider stock size, tool access, standard hole sizes, corner radii, and potential process consolidation before machining begins. Early design-for-machining feedback can reduce avoidable revisions, although the final improvement depends on the drawing quality and project complexity.
A Practical Selection Framework
Step 1: Define the Functional Requirement
Start by describing what the component must do, not only how it looks. State whether it locates, supports, guides, transfers, clamps, protects, or connects other parts, and identify the most important contact surfaces. Include the operating environment, expected handling method, cleaning exposure, and any interaction with sensors, robots, conveyors, or fasteners.
Step 2: Separate Critical and Non-Critical Features
Mark the datums, mounting holes, locating pins, sealing surfaces, and other features that directly affect assembly or motion. Apply tighter tolerances only where they are technically necessary and leave general dimensions at practical levels where possible. This approach gives the machinist a clearer inspection priority and can help control both machining time and measurement effort.
Step 3: Review Manufacturability Before Quotation
Deep pockets, very thin walls, sharp internal corners, long slender features, and inaccessible holes can increase tool deflection or require additional setups. I review these features before quotation because a small drawing change may improve rigidity or permit more efficient tooling. A design that can be machined in fewer setups may also reduce the number of datum transitions that need to be controlled.
Step 4: Confirm Material, Finish, and Inspection
Specify the alloy and temper, required certificates if applicable, surface treatment, deburring expectations, and inspection documentation. If the part will be anodized, clarify color, masking, coating thickness expectations, and post-finish critical dimensions. For inspection, identify whether a dimensional report, first-article inspection, thread verification, or customer-specific format is needed.
Pricing, Quantity, and Lead-Time Considerations
Prototype pricing is influenced by programming, material preparation, setup count, machining time, tooling, finishing, inspection, and packaging. The part quantity matters, but it is not the only cost driver; a single complex component may require more engineering and setup work than several simple brackets. Buyers can obtain a more useful quotation by sending a 3D model, a 2D drawing, material requirements, finish details, quantity, and target schedule together.
Lead time should be quoted after the supplier has reviewed material availability, drawing completeness, outside processing, and inspection requirements. I avoid presenting a universal delivery promise because these factors vary significantly between projects. If a test date is fixed, tell the supplier early and ask for a production plan that separates drawing review, material preparation, machining, finishing, inspection, and shipment.
How to Evaluate an Aluminum Machining Supplier
Technical and Quality Questions
Ask whether the supplier has experience with aluminum fixtures, pallet components, and material handling interfaces similar to your part type. Review how they handle drawing revisions, critical dimensions, burr control, thread protection, surface treatment, and nonconformance communication. A credible supplier should explain what information is needed to quote accurately rather than accepting an incomplete specification without clarification.
Also assess whether the supplier can coordinate secondary operations and provide the inspection records your project requires. If a part has critical positional relationships, ask how datums are established and how those relationships will be verified. I recommend checking sample documentation and communication quality during the quotation stage, while avoiding assumptions about capability that have not been confirmed for the specific component.
Commercial and Project Support
For a prototype project, responsive engineering communication can be as important as the machining equipment. Changes to hole size, finish, material, or tolerance may occur after the first review, so a clear revision-control process helps prevent outdated files from entering production. Packaging should also be discussed when anodized faces, precision locating surfaces, or delicate edges must be protected during transport.
At Cornerstone, we support buyers by reviewing aluminum prototype machining requirements for pallet and material handling applications, clarifying manufacturability questions, and coordinating machining with requested finishing and inspection steps. Our role is to help convert a design file into a practical, traceable manufacturing plan. The exact process, tolerance capability, finish, documentation, and schedule should be confirmed for each drawing before an order is placed.
Key Takeaways
- Choose aluminum grade and temper according to load, environment, finishing, and joining requirements.
- Use CNC machining for prototypes that need accurate interfaces, functional testing, and design flexibility.
- Identify datums and critical features instead of applying unnecessarily tight tolerances to every dimension.
- Review thin walls, deep pockets, sharp corners, and difficult setups before requesting a quotation.
- Provide the 3D model, 2D drawing, quantity, finish, inspection needs, and target date in the initial inquiry.
- Evaluate suppliers on technical review, revision control, inspection communication, and secondary-process coordination.
Conclusion and Next Steps
Aluminum prototype machining is a practical route for validating pallet and material handling equipment components before larger production commitments. The strongest results come from connecting the application requirement to the material, geometry, tolerance, finish, and inspection plan. It is not enough to request “an aluminum prototype” without defining the interfaces and conditions that determine whether the part will function.
To begin, prepare your 3D model, 2D drawing, alloy and temper preference, quantity, surface finish, critical dimensions, inspection expectations, and required delivery date. Send those details to Cornerstone for a manufacturability review and quotation discussion. We can then help determine a suitable machining approach and identify open technical decisions before production starts.
If you want to learn more, please visit our website aluminum prototype machining.

Comments
All Comments ( 0 )